


Objective
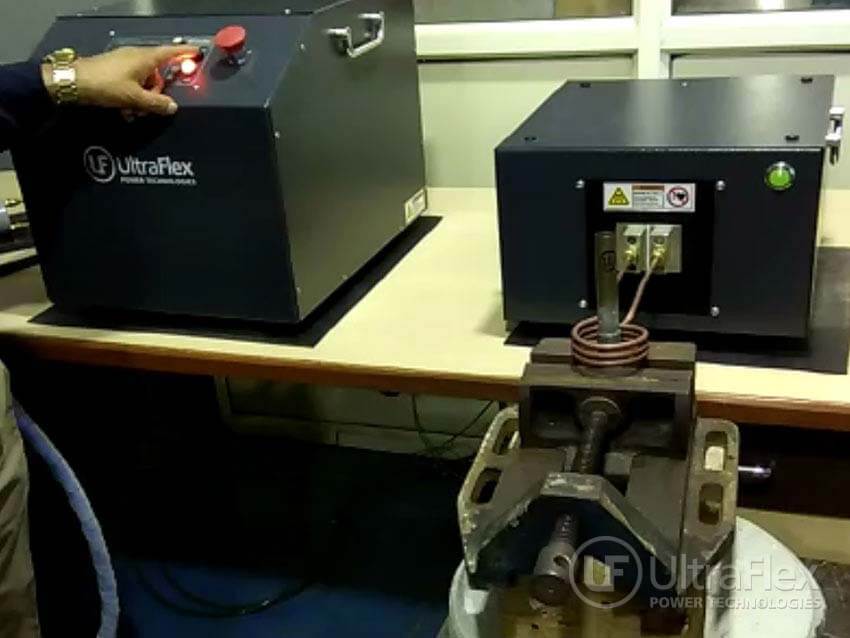
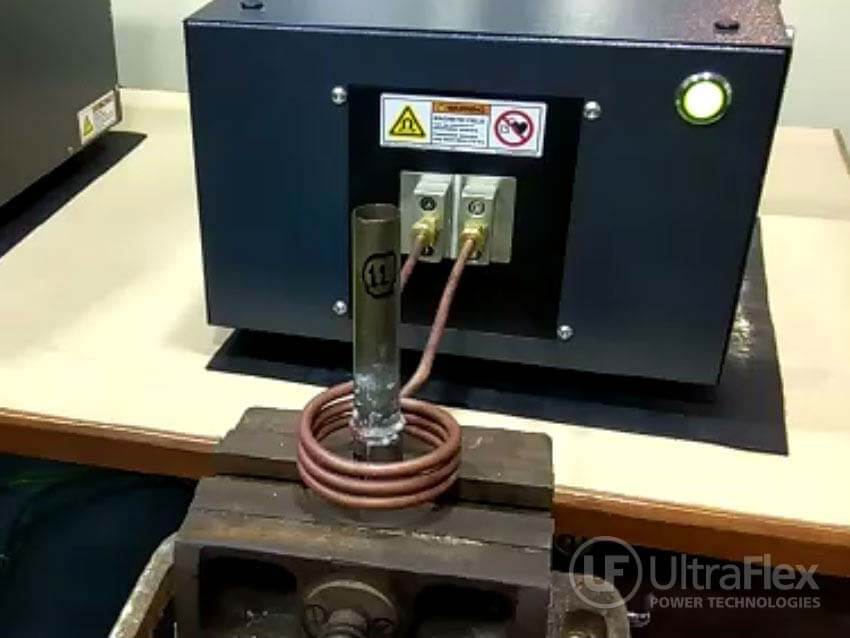
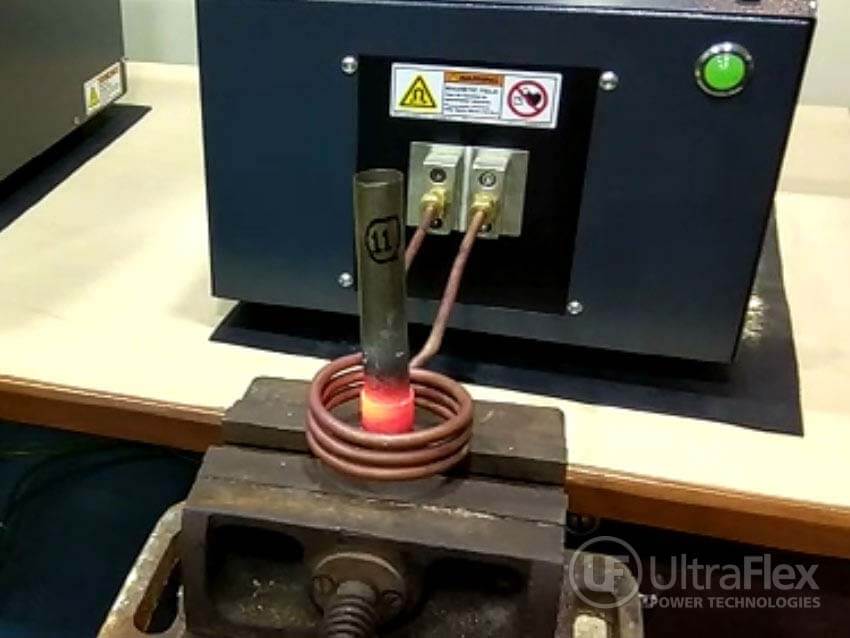
The purpose of this test is to braze a tube to a tube end assembly.
Materials
Tube length varies from 39.3″ (1m) to 236.2″ (6 m).
Key Parameters
Temperature: Around 1382°F (750°C)
Time: 1 minute to 30 seconds average
Results and Conclusions:
The tube end length varies from the present 1.57″ to 3.94″ (40mm to 100 mm), and the perforated tube length varies from 3.28ft to 19.685ft (1m to 6 m). The lap Joint length may reach up to a maximum of 0.28″ (7 mm) in the future.
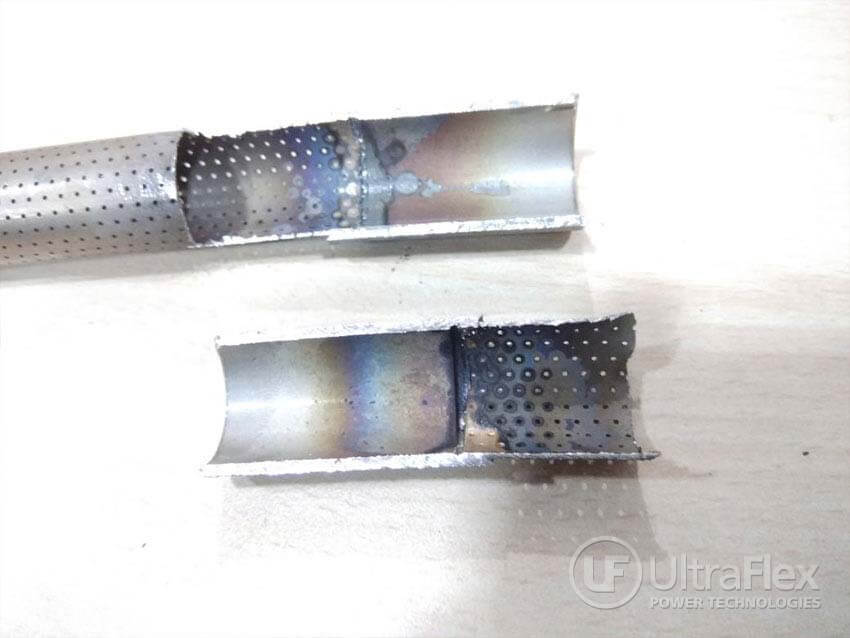
Quality requirements: Lap joint, all holes, joint line at the inside end of the lap, and joint line on the OD of the tubes should be completely suffused with brazing filler.
The joint has physical strength requirements also.
You will suggest the final parameters, as well as flux and filler metal requirements for a proper brazed joint & fixtures, if any.
Final tube outer diameters will reach up to 1.97″ (50 mm). The length will not differ much. Perforated tube thickness may reach up to 0.079″ (2 mm) maximum.
Pictures


Subscribe to our YouTube Channel:
Video
Request information or contact us about this application. Reference info: Application Note 3463-4915
